Featured Contract Production Collections
Engineered to international optical dispensary tolerances. Our production lines combine artisanal hand-polishing and multi-axis automated milling for private label optical brands, luxury eyewear retail chains, and international distributors.
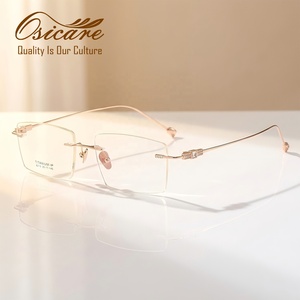
Premium Women Rhinestone Diamond Glasses Luxury Eyewear Titanium Rimless Decor Frames
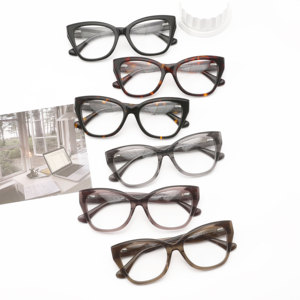
Oversized Eyeglasses Cat Eye Acetate Optical Frames Ladies Spectacle Frames
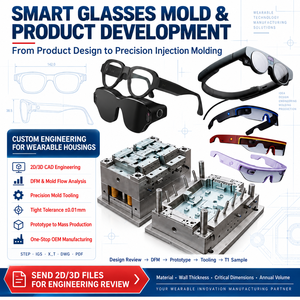
High-Precision Injection Mould for Optical Lenses Custom Multi-cavity VR/AR Glasses Equipment
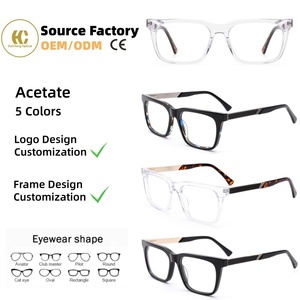
Customization High-end Handcrafted Acetate Optical Glasses Durable Rectangle Eyeglasses Frame
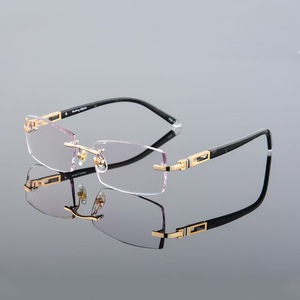
Custom Rectangle Gradient Tint Plano Prescription Frame Alloy Diamond Trimming Rimless Glasses
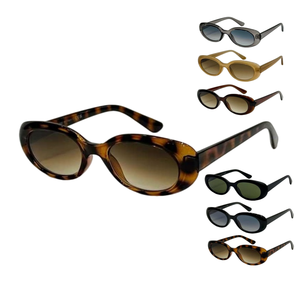
Italy High Quality Trending Acetate Glasses Luxury Eyewear Kit Designer Sunglasses Square-Round
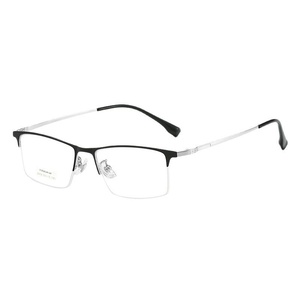
Ultra-light Beta Titanium Semi-rimless Square Eyeglass Frame Business Smart Optical Glasses
75+
Years Heritage Pedigree
3,000+
Daily Finished Capacity
1,000+
Bespoke SKUs / Year
90+
Export Destination Markets
0.02mm
CNC Micro Machining Limit
Navigating Eyewear Contract Manufacturing: The Modern Sourcing Paradigm
Evaluating high-yield manufacturing partnerships in optical framing requires an analytical assessment of material supply chains, mold micro-tolerances, surface plating durabilities, and turnkey assembly reliability. Here is how modern contract production creates undeniable commercial advantage.
Full Vertical Integration
Decoupled production chains lead to critical tolerance stack-ups, mismatched color lot variances, and hinge torque inconsistencies. Our facility integrates CAD structural mechanics, mold design, raw acetate block curing, CNC profiling, high-vacuum IP galvanic plating, and lens edging under a singular engineering protocol.
By controlling all fabrication phases from 3D parametric blueprints to ultrasonic cleaning and final optical alignment, we eradicate supply chain middle-tier margins while guaranteeing deterministic batch-to-batch repeatability.
- Elimination of subcontractor handoff variances
- In-house multi-cavity injection mold tooling
- Proprietary multi-stage tumbling & hand-buffing
Medical & Optical Compliance
Global regulatory landscapes require comprehensive documented conformity for optical frames and ophthalmic instruments. We maintain ISO 9001 certified quality management protocols, delivering rigorous batch conformity to European CE EN ISO 12870, UKCA standards, and US FDA Class I 510(k) exemptions.
Our raw formulations pass rigorous biocompatibility testing, ensuring 100% hypoallergenic skin-contact safety without free lead, hazardous cadmium, or leachable nickel migration under EN 16128 sweat corrosion testing.
- Nickel-release compliant under EN 16128 (<0.5 μg/cm²/week)
- REACH Regulation (EC) No 1907/2006 compliant
- FDA registration & Drop Ball impact certified
IP Protection & Discretion
Private label innovation is highly vulnerable to industrial leakage. Originating from historic Italian heritage principles where brand exclusivity is sacred, our manufacturing environment enforces strict physical and digital NDAs across all client product development pipelines.
Proprietary eyewear silhouettes, unique crystal setting patterns, customized hinge ergonomics, and custom acetate lamination codes remain strictly cordoned within isolated CAD/CAM servers, preventing counterfeit leakage into wholesale open markets.
- Encrypted CAD/CAM blueprint security
- Exclusive custom tooling ownership models
- Isolated prototyping & clean-room sampling
Comparative Manufacturing Capabilities Matrix
We operate distinct manufacturing units specialized in primary ophthalmic materials, ensuring structural equilibrium, mechanical durability, and aesthetic luxury.
| Material Technology | Primary Substrates | Fabrication Tolerance | Finishing & Surface Treatment | Typical Applications | Key Buyer Benefit |
|---|---|---|---|---|---|
| High-Grade Cellulose Acetate | Cotton-derived bio-acetate, Mazzucchelli block formulations (3mm to 12mm) | ±0.05 mm via 5-axis CNC router | 72-hour walnut & pumice barrel tumbling, high-luster hand-wheel buffing | Luxury designer sunglasses, bold retro spectacles, handcrafted opticals | Deep tactile warmth, organic flex memory, hypoallergenic face contact |
| Beta-Titanium & Pure Ti | JIS Grade 2 Pure Titanium, β-Ti 15-3-3-3 alloy wire & sheet plate | ±0.02 mm CNC micro-wire EDM & stamp | Vacuum IP (Ion Plating), PVD coating, micro-laser spot welding | Executive business eyewear, ultra-light semi-rimless frames, flexible temples | Sub-8g weight, extreme elasticity, zero nickel corrosion over lifespan |
| High-End Optical Alloys | Monel, nickel-silver, stainless steel 304/316L, architectural beryllium copper | ±0.03 mm high-speed stamped | Electrophoretic coating, 18K/24K gold flash dip, galvanic protective seal | Cat-eye frames, diamond-cut rimless spectacles, jewel-adorned frames | Rigid dimensional stability, complex profile contours, jewel-setting support |
| Precision Optical Injection | EMS TR90, Ultem (PEI), Arkema Rilsan® Clear G850 Bio-Polyamide, PC | ±0.002 mm high-cavity mold | Soft-touch rubberizing, anti-scratch hard coat, gradient robotic spray | Active sports eyewear, smart audio frames, AR/VR optical chassis | High tensile fracture resistance, featherweight volume scaling, low unit cost |
Future Procurement Trends in Global Eyewear (2025–2030)
Strategic eyewear category managers must anticipate paradigm shifts across sustainable material science, hybrid smart hardware integration, and demand-responsive agile manufacturing cycles.
1. Circularity & The Bio-Acetate Imperative
Consumer scrutiny and ESG compliance mandates across the European Union (such as the Corporate Sustainability Due Diligence Directive) are transforming optical material procurement. Traditional cellulose acetate utilizes diethyl phthalate (DEP) plasticizers, which face accelerating regulatory phase-outs.
Our production facilities lead this transformation by converting contract lines to certified Bio-Acetate formulated from sustainably harvested wood pulp and cotton linters plasticized with bio-based ester derivatives. These compounds achieve 68% to 115% bio-based carbon content according to ASTM D6866 and achieve complete biodegradation under ISO 14855 industrial composting parameters without degrading dimensional stability or color vibrance.
Contract buyers partnering with our production lines secure verifiable FSC chain-of-custody documentation, granting direct competitive advantage in Tier-1 North American and European retail shelves.
2. Spatial Computing & Smart Eyewear Convergence
The boundary between traditional ophthalmic frames and smart spatial hardware has disintegrated. Eyewear brands are no longer sourcing purely static frames; they require contract manufacturers capable of engineering hybrid structural architectures that integrate micro-optics, wave-guides, compact PCB cavities, capacitive touch temples, and lithium micro-battery pockets.
As demonstrated by our proprietary High-Precision VR/AR Mold Lines, our tooling division mills multi-cavity injection matrices yielding surface roughness tolerances under Ra 0.05 μm. This allows direct co-molding of conductive flex circuits and optical prisms into ultra-dense, featherweight TR90/PEI frames without thermal warping.
Forward-thinking brands are utilizing our R&D engineering cells to prototype smart prescription platforms that appear as refined as high-end Italian spectacles while functioning as everyday connected wearables.
3. Micro-Weight Structural Engineering (Titanium & Rimless)
Ergonomic wearability has become a primary driver of recurring purchase intent among optical consumers. Heavy frames that induce nose bridge fatigue or temple pressure points are rapidly losing market share to sub-10g silhouettes. This consumer transition is surging demand for Beta-Titanium Semi-Rimless and Diamond-Cut Frameless constructions.
Machining β-titanium demands specialized wire-EDM cutting, cold-stamping, and inert atmosphere laser welding to prevent micro-fissures and thermal embrittlement. Our automated tooling suites achieve exceptional flexibility, enabling ultra-thin 0.8mm temple arms that maintain clamping force memory over 30,000 continuous hinge flexes.
For rimless diamond-trimming designs, our CNC diamond cutters facet prescription lenses with laser-guided edge chamfers, allowing jewel settings and structural bridge mountings that resist torque cracking during ophthalmic glazing.
4. Agile MOQs & Accelerated Prototyping
The era of rigid 5,000-piece minimum order quantities per colorway is obsolete. Eyewear brands operating modern omnichannel models demand high-frequency collection drops, localized capsule lines, and minimized capital tie-up. Sourcing managers now require contract manufacturing partners that balance high-volume scale with flexible short-run sampling.
By leveraging in-house rapid prototyping, 3D wax SLA printing, and modular mold tooling, our factory compresses sample turnaround from the conventional 45 days down to just 10 to 14 business days. This empowers private label brands to test retail appetite with agile 300–500 piece pilot runs before initiating mass automated production.
This structural agility shields brands against inventory obsolescence while ensuring uninterrupted inventory re-order cycles calibrated precisely to real-time point-of-sale data.
From Design Blueprint to Global Freight Delivery
Our systematic 5-stage production methodology ensures absolute transparency, documented milestones, and zero margin for manufacturing error.
Stage 01
Technical CAD & DFM
Conversion of styling sketches into 3D parametric CAD files. Design for Manufacturing (DFM) audits optimize bridge thickness, pantoscopic tilt, and screw retention stability.
Stage 02
Rapid Functional Prototyping
SLA 3D master prints and CNC-machined physical acetates are rendered within 10 days for ergonomic validation, face-fit ergonomics, and mechanical balance assessment.
Stage 03
Precision Tooling & Setup
In-house CNC mold cutting, EDM electrode engraving, custom temple wire-core dies, and high-precision stamping fixtures prepared with tolerances to ±0.002mm.
Stage 04
Mass Fabrication & Finish
Automated cutting, tumbling, manual artisanal wheel buffing, vacuum ion-plating, and robotic ultrasonic cleansing achieving mirror-gloss optical dispensary grade finishes.
Stage 05
100% Optical QA & Logistics
Every single frame undergoes 12-point inspection: hinge torque testing, sweat immersion check, lens retention verification, laser logo etching, and direct export dispatch.
Frequently Asked Questions by Eyewear Buyers
Direct technical and commercial answers addressing common international procurement concerns regarding MOQs, compliance protocols, tooling amortization, and lead times.
What is the minimum order quantity (MOQ) structure for custom OEM/ODM production? +
Our MOQ structure is engineered to accommodate both emerging designer brands and tier-one retail conglomerates. For custom handmade cellulose acetate frames, our baseline MOQ is 300 pieces per model, which can be split across 2 to 3 custom colorways (e.g., 100 pcs Classic Black, 100 pcs Havana Tortoise, 100 pcs Crystal Clear). For titanium and alloy metal wire-frame programs, the standard run is 300 pieces per SKU due to plating jig setups. For high-volume precision injection-molded eyewear (TR90, Ultem, or VR equipment), the initial minimum is 600–1,000 units to offset automated mold cycling efficiencies. For established enterprise programs, we provide rolling buffer inventories and annualized master-agreement call-offs.
How does your factory verify adherence to international compliance standards (CE, FDA, UKCA)? +
Every optical frame and sunglasses series leaving our facility is accompanied by full Declaration of Conformity (DoC) documentation. We execute certified laboratory testing verifying European Standard EN ISO 12870 (Ophthalmic optics — Spectacle frames) requirements, including bridge deformation endurance, optical lens retention under stress, endurance fatigue resistance after 500 cycles of bridge flexing, and high-temperature environmental aging. For sunglasses, our lenses meet EN ISO 12312-1 and ANSI Z80.3 requirements for UV400 spectral cutoff, optical clarity, and Drop Ball impact resistance. We maintain valid FDA Device Facility Registrations and ISO 9001 certified manufacturing audits ready for institutional verification.
What are the standard sample development and mass production lead times? +
Our vertically integrated layout significantly compresses standard industry turnarounds. 3D technical CAD layouts are delivered within 48 to 72 hours from your initial technical pack or concept reference. Functional physical samples machined from stock raw acetate blocks or 3D SLA resins take 10 to 15 calendar days. Bespoke tooling for custom stamped metal temples or injection molds requires approximately 25 to 30 days. Once pre-production gold-seal prototypes are approved, mass manufacturing lead times typically span 45 to 60 calendar days, depending on material complexity (e.g., multi-layer hand-laminated acetate requiring stabilizing curing ovens versus rapid-cycle injection frames).
Who owns the tooling, injection molds, and proprietary industrial design rights? +
Tooling and mold assets paid for by the client remain 100% the intellectual and physical property of the client. Upon completion of mold amortization or direct payment, a formal Intellectual Property & Mold Custody Agreement is executed. We assign a unique identification code to your tooling, maintain it without added fees throughout production lifecycles, and guarantee that client molds will never be used to manufacture frames for any third-party brand or open wholesale distributor. Clients are entitled to retrieve or transfer their molds at any time upon formal notice.
Can you provide custom acetate patterns and proprietary color laminations? +
Yes. In addition to sourcing world-renowned raw sheet stocks from premium Italian and Asian houses (such as Mazzucchelli 1849 and Jimei), our internal chemical and thermal bonding department produces bespoke custom acetate laminations. We engineer multi-tone sandwiched laminates, embedded wire-core textures, etched logo cores, and bespoke tortoise patterns. Custom acetate block production requires minimum batch sheet casts of roughly 30–50 kg, which our engineering team seamlessly integrates into your seasonal development calendar to guarantee exclusive colorway protection.
How does your quality control department manage hinge torque stability and surface plating longevity? +
Surface plating durability is tested in-house via a 48-hour continuous neutral salt spray chamber (ASTM B117 / ISO 9227) and artificial perspiration immersion under EN 16128 to confirm absolute resistance to blistering, discoloration, or galvanic corrosion. Frame hinges (from traditional 3-barrel and 5-barrel riveted hinges to high-end OBE/Comotec spring mechanisms) are tested using automated cycle testers that open and close temples for 20,000 cycles under calibrated resistance to ensure smooth torque tension retention without screw loosening or structural play.
What packaging, branding, and private label optical kit solutions are supported? +
We provide complete, retail-ready turnkey packaging solutions. This includes high-definition fiber laser logo etching on inner temples and demo lenses, pad printing, hot foil stamping, and metal temple-end cast inlays. Beyond the frame itself, our contract capabilities encompass bespoke origami folding cases, recycled PU leather hard cases, certified rPET microfiber lens cloths, retail presentation boxes with magnetic closures, tamper-evident barcoding, and multilingual user manual inserts compliant with international consumer retail laws.
How do we initiate our first RFQ (Request for Quotation) and sample batch? +
Initiating a technical review is straightforward. Simply click our inquiry interface below to transmit your design tech packs, 2D vector sketches, or physical reference frame parameters along with your anticipated volume projections. Our senior optical engineering team will review your specifications within 24 hours, providing a detailed DFM analysis, line-item tooling breakdown, unit pricing tiers, and a precise prototype development timeline.
Scale Your Eyewear Brand with Industrial Production Excellence
Partner with an established contract manufacturer providing European craftsmanship standards, medical-grade optical compliance, and dependable high-volume output. Submit your project requirements to consult with our technical production team today.